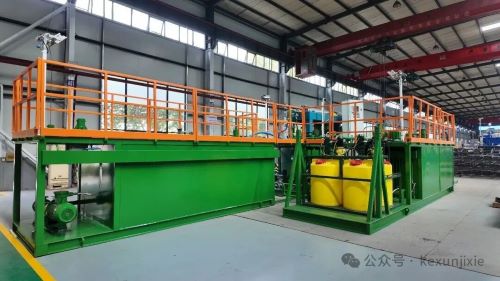
Welcome! Black Rhino proudly presents our fully integrated, commission-ready Oily Sludge Treatment System with a processing capacity of 1 ton per hour. This system has successfully passed all factory acceptance testing (FAT) and is prepared for immediate shipment to the client’s project site.
Project History and Core Objectives
This specialized system was custom-engineered for a waste oil recycling enterprise operating in Africa. The client focuses on the collection and disposal of oily sludge from both onshore and offshore oilfields. For an extended period, traditional waste incineration was deployed at this facility. This method incurred massive operational expenses and imposed a heavy environmental liability. The client established clear project metrics: high-efficiency recovery of commercial-grade oil, complete purification of recycled process water, and maximum volume reduction of the dry solid cake.
Technological Process and Three-Phase Separation Layout
Black Rhino specialists engineered a complete turnkey solution. The system seamlessly integrates modules for conditioning, thermal heating, chemical dosing, three-phase centrifugal separation, recovered oil storage, and automated PLC control.
The process leverages thermal-chemical washing paired with advanced centrifugal separation:
- Conditioning Phase: The raw oily sludge is transferred into the technological conditioning reservoir. High-temperature steam, specialized chemical reagents, and intensive agitation disrupt the colloidal structure of the emulsion, completely stripping hydrocarbons from the surfaces of the solid sludge particles.
- Three-Phase Separation: The conditioned slurry is transferred via a feed pump into the Black Rhino LWS350 three-phase decanter centrifuge. Utilizing differential densities under high centrifugal G-force, the unit achieves continuous, clean separation of all constituent phases.
- Closed-Loop Recovery: The isolated liquid oil phase is routed directly to storage tanks for immediate commercial reuse. The purified water stream is fully recycled back into the thermal-chemical washing phase. The isolated solid discharge is evacuated with minimal oil and moisture content, ensuring safe transport to a landfill.
The fully closed-loop process water recycling loop completely eliminates the need for a continuous freshwater supply. This delivers a critical operational advantage in arid African environments.
System Configuration and Modular Construction
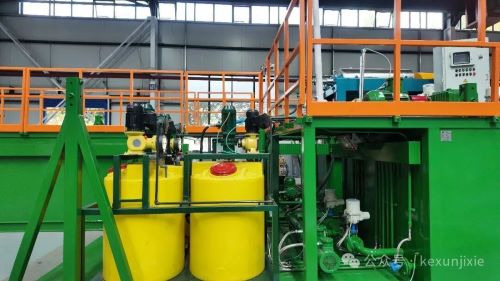
The complete processing line is engineered across six core blocks: the conditioning module, centrifugal separation module, oil storage module, automated chemical dosing unit, thermal heating module, and the central control station. The entire system features a heavy skid-mounted design. All units are pre-assembled on durable steel skids at the Black Rhino production facility. This configuration eliminates the need for complex concrete foundations and guarantees rapid commissioning at the project site.
Key Engineering Advantages of the Black Rhino System:
Field-Proven Design for Harsh Climates: All electrical components feature robust explosion-proof ratings. Structural steel assemblies are protected with multi-layer anti-corrosion coatings. The system operates stably under extreme ambient temperatures and frequent sandstorms.
Economic Viability: The exceptional quality of the recovered oil allows for immediate reintegration into the production stream. This offsets waste management costs and generates an additional corporate revenue stream.
Maximum Waste Volume Reduction: Deep centrifugal dewatering drastically shrinks the total volume of the solid cake, lowering transportation and hazardous waste disposal fees.
Operational Versatility: The machinery stably processes diverse feedstocks. The system efficiently treats pit sludge, crude storage tank bottoms, drilling muds, and oil-based drill cuttings.
Full PLC Automation: Equipped with an integrated PLC control cabinet, the system supports continuous 24/7 unmanned operations. Core processing parameters are monitored remotely, minimizing required on-site headcount.